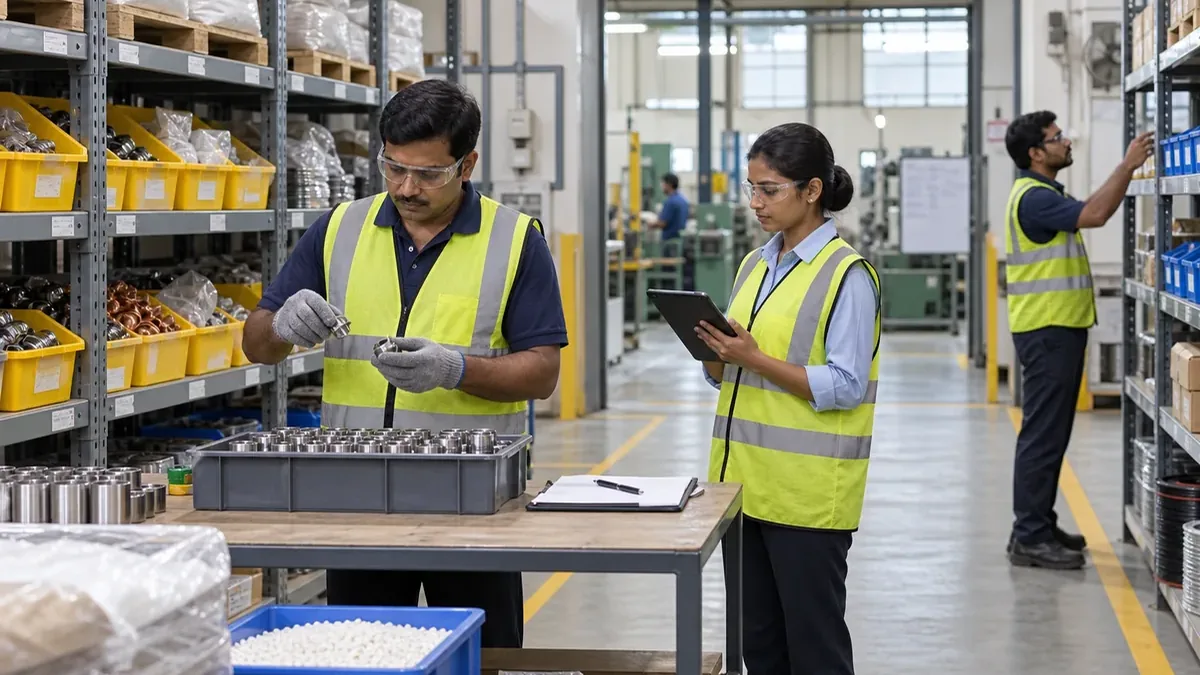
Manufacturing stock control software should help a factory answer more than how much material appears in the system. It should show whether that balance can be trusted, when it was last checked, what movement caused a difference, and who approved a correction.
A full physical stocktake can interrupt normal work and still leave teams with a long list of unexplained adjustments. Cycle counting divides that work into smaller, planned counts throughout the operating calendar. The goal is not to make variances disappear on paper. It is to find process failures early and improve the records used by purchasing, production, quality, and dispatch.
Start with the inventory foundation
Reliable counting depends on clean item codes, units of measure, storage locations, stock statuses, and movement rules. One material should not appear under several informal names. A kilogram, piece, metre, coil, or box must have an agreed conversion where more than one unit is used.
Before configuring cycle counts, review the broader inventory management software foundation. Separate raw material, work in progress, finished goods, rejected stock, customer material, and supplier-owned stock according to the factory's real responsibilities. A count cannot correct an unclear ownership or status rule.
Define what a count covers
Each count task should identify the item, location, lot or batch when applicable, stock status, unit, planned date, and assigned counter. Decide whether sealed packs can be accepted by quantity or must be opened, and how partially used containers, cut lengths, remnants, returnable items, and material at machines will be handled.
Do not combine several stores into one count line. A correct total can hide material recorded in the wrong rack or status. Location-level counting exposes misplaced stock and makes the next issue or pick easier to perform correctly.
Set a practical counting frequency
Count frequency should reflect operational risk, not only item value. Consider movement frequency, production criticality, shortage impact, handling difficulty, past variance, expiry or shelf-life controls, and whether the item is easy to confuse with another code.
Use a simple classification the team can explain. Frequently moved or production-critical materials may be checked more often; stable, low-risk items may be checked less often. Review the classification when usage patterns, suppliers, layouts, or product mixes change. Avoid treating an old ABC list as a permanent rule.
Create a balanced count schedule
Spread tasks across working days and storage zones so stores staff can complete them without neglecting receipts and production issues. Avoid scheduling a difficult rack, a high-volume receipt window, and a shift change at the same time. Include overdue tasks and repeatedly inaccurate items in the supervisor's daily view.
A factory stock management software workflow can propose tasks from the policy, but a responsible person should approve changes to frequency, scope, or due date. Record why a task was postponed rather than silently moving it forward.
Control movements during the count
Before counting, define a cutoff. The item and location may be temporarily frozen, or every receipt, issue, transfer, return, and production movement during the count must be logged and reconciled. The suitable method depends on how long counting takes and whether production can pause access.
Display the count status to users who create stock movements. If urgent material must be issued, capture its time, quantity, source, destination, and authorisation. A physical quantity observed at one time cannot be compared fairly with a system balance from another time.
Use blind counts where useful
A blind count hides the expected system quantity from the counter. This reduces the temptation to make the physical result match the screen without checking. The counter records the observed quantity, unit, time, location, and any condition such as damaged packaging, mixed items, or an unreadable label.
For weighed, measured, or estimated material, record the method and equipment used. Where safety or material handling requires two people, the workflow should support a counter and witness. Photos may help document unusual conditions, but they should not replace a recorded quantity and decision.
Route differences to investigation
When physical and system quantities differ, put the line into a variance status. Do not immediately overwrite the balance. The system should preserve expected quantity, counted quantity, difference, value basis where authorised, counter, timestamp, and supporting notes.
Set recount rules according to the factory's control policy. A second person can recount without seeing the first result. The workflow should distinguish a counting mistake from a confirmed stock difference and show which step is waiting for action.
Investigate the movement trail
Review recent receipts, quality releases, production issues, returns, transfers, dispatches, scrap, and adjustments. Check for delayed entries, wrong locations, incorrect units, duplicate postings, backdated transactions, mixed lots, unrecorded returns, and material still lying near a machine.
Connect the investigation with job card records when material was issued to production, and with batch and lot traceability when identity matters. The purpose is to locate the failed transaction or process step, not to assign blame without evidence.
Approve controlled stock adjustments
A confirmed difference may require an adjustment, but the adjustment should have a reason, approver, effective time, reference to the count, and a clear before-and-after balance. Separate permissions for counting, investigating, and approving important adjustments where the team size allows it.
Never delete the original count or movement history. If an approval is rejected, retain the decision and return the task for clarification. Lock completed adjustments from casual editing and use a reversal or authorised correction process when a later error is found.
Turn variance reasons into prevention
Use a short, controlled reason list such as receipt not posted, issue not recorded, wrong location, unit conversion, mixed item, scrap not recorded, production return missing, transfer incomplete, label problem, or counting error. Allow notes for context without creating dozens of nearly identical categories.
Review recurring causes by item, location, shift, transaction type, and process owner. A pattern of wrong-location differences may call for better rack identification or transfer discipline. Repeated missing issues may require a simpler shop-floor transaction, clearer responsibility, or a connection to the production record.
What manufacturing stock control software should show
The counter needs a focused task list, location and item identity, unit, count-entry controls, observation notes, and offline handling where connectivity is unreliable. The supervisor needs due and overdue tasks, frozen locations, open variances, recounts, investigations, pending approvals, and exceptions affecting production.
The management view should show count completion, unresolved differences, recurring causes, and actions, with links to source records. The manufacturing dashboard guide can help keep this view centred on decisions instead of decorative totals.
Pilot one stores zone
Choose one bounded zone with known items and an involved stores team. Clean the item and location masters, define frequency and cutoff rules, assign responsibilities, and prepare count, recount, investigation, approval, and correction scenarios before the pilot begins.
Test normal counts, zero stock, excess stock, short stock, mixed items, wrong location, open receipt, urgent issue during counting, rejected material, a failed device connection, an overdue task, and an authorised reversal. Compare system records with direct observation until the workflow is clear.
Select software around traceable decisions
Evaluate item and location controls, lot and status handling, flexible scheduling, blind counts, movement cutoff, recounts, variance workflow, approval permissions, audit history, offline behaviour, exports, backups, and links to purchasing and production. Ask vendors to demonstrate your actual exception cases with representative data.
Useful stock control software does not merely change a number after a count. It makes the difference visible, guides investigation, records the authorised decision, and helps prevent recurrence. Start with one zone and a disciplined daily rhythm, then expand when the team trusts the process.
Want to map a controlled cycle-count workflow?
Share your item list, stores layout, stock register, count sheet, and adjustment approval process. Ploqy Technologies can help structure a focused workflow around counting, movement control, variance investigation, approvals, and practical daily review.
Continue with a related guide
- Inventory Management Software for Small Manufacturers: A Practical Guide
- How Material Shortage Alerts Prevent Production Delays
- MRP Software for Small Manufacturers: A Practical Setup
Manufacturing software servicesManufacturing website servicesDownload the project checklist
Published by Ploqy Technologies. About our guides and editorial process.